Power Adapter·Ultrasonic Welding Machine·AC/DC Cable Harness Customization | Winna Technology
Home page
About Us
Exhibition
AC/DC Cable Harness
All
Cable Harness Cases
Equipment Certification
Customization Capability
Product Center
Wire Harness FAQ
Ultrasonic Metal Welding
All
Accessories and Consumables
Device Center
Case
Ultrasound FAQ
Power Adapter
All
Product Center
Custom Submission
Certification/Equipment
Power Adapter Cases
Adapter FAQ
Technical Resources
All
Adapter Technology Resources
Ultrasonic welding technology resources
Wire Harness Technical Resources
Contact us
Submit requirements
Download Center
Sample Application
Privacy Policy
Careers
EN
CN
DE
ES
JP
TH
VI
Case
Your location
Home page
Ultrasonic Metal Welding
Case
Ultrasonic Battery Tab Welding | Lithium Battery Cell Electrode Welding
2026-08-05 00:00:00
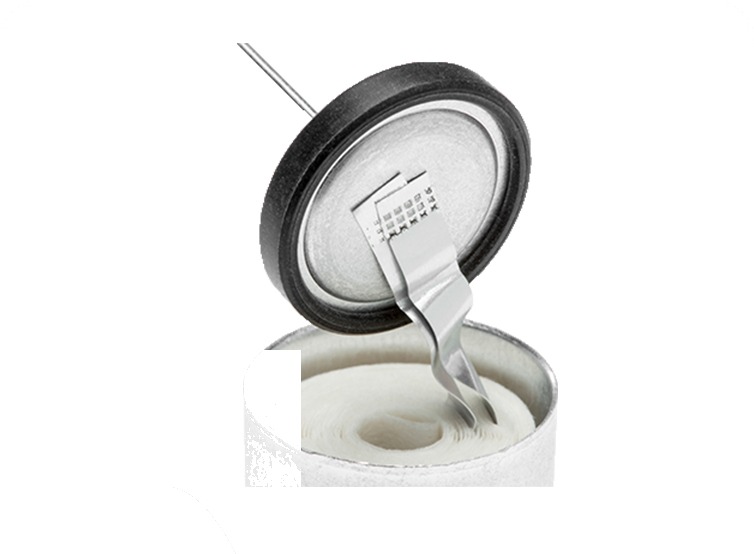
.welder-sample{font-size:15px;line-height:1.85;color:#374151;max-width:900px} .welder-sample h3{font-size:18px;font-weight:600;color:#111827;margin:28px 0 12px;padding-left:14px;border-left:3px solid #DC2626} .welder-sample p{margin:0 0 14px} .welder-sample .spec-box{background:#F9FAFB;border-radius:10px;padding:18px 22px;margin:16px 0;border-left:3px solid #DC2626} .welder-sample .spec-box strong{color:#111827} .welder-sample img{max-width:100%;height:auto;border-radius:10px;margin:8px 0;box-shadow:0 2px 12px rgba(0,0,0,0.08)} .welder-sample .img-grid{display:grid;grid-template-columns:1fr 1fr;gap:12px} .welder-sample .img-grid img{width:100%;height:auto;margin:0} .welder-sample .tag{display:inline-block;background:#FEF2F2;color:#DC2626;font-size:12px;font-weight:600;padding:2px 10px;border-radius:10px;margin-right:4px} @media(max-width:768px){.welder-sample .img-grid{grid-template-columns:1fr}} 焊接类型 超声波电池极耳焊接(Ultrasonic Battery Tab Welding)—— 将电池极片多层箔材(铝箔/铜箔)与极耳(铝极耳/镍极耳)通过超声波振动实现固态焊接,是锂电池电芯制造中的核心工艺环节。 工艺参数: 频率20kHz | 焊接功率1500~2500W | 焊接时间0.2~0.4s | 振幅35~55μm 适用极片: 铜箔(8~20μm)×多层 + 镍极耳(0.1~0.3mm) 铝箔(12~20μm)×多层 + 铝极耳(0.1~0.3mm) 焊接效果: 焊合率≥95% | 剥离强度≥极耳本体强度80% | 焊后极片无裂纹 工艺优势 电池极耳焊接对精度和一致性要求极高——焊点过深会损伤极片导致内短路,焊点过浅则内阻超标。我司焊接设备采用实时能量补偿技术(RTC),在连续生产中保持每次焊接能量偏差<±3%。配合CCD视觉定位系统,极耳对位精度可达±0.1mm,满足动力电池和储能电池的严苛工艺要求。 适用电芯类型:圆柱电池(18650/2170/4680)、方形铝壳电池、软包电池。 ▼ 电池极耳焊接样品实物图展示
No more
No more