


Ultrasonic Welding vs Crimping for Wire Harness: 5 Key Advantages
Explore the 5 key advantages of Ultrasonic Welding vs Crimping for Wire Harness to optimize your wire connection process, enhance reliability and production eff
Against the backdrop of rapid expansion in the new energy vehicle and energy storage industries, the reliability of wire harness connection processes directly determines the safety performance and service life of the entire vehicle. Ultrasonic metal welding machines achieve solid-state metallurgical bonding through high-frequency mechanical vibration, and are becoming the mainstream choice to replace traditional crimping processes. This article systematically compares the differences between ultrasonic welding and crimping processes from five dimensions: technical principles, product selection, specification analysis, application validation, and procurement decision-making, providing a complete technical reference for B2B engineering decision-makers.
Product Overview: Technical Positioning and Process Value of Ultrasonic Metal Welding
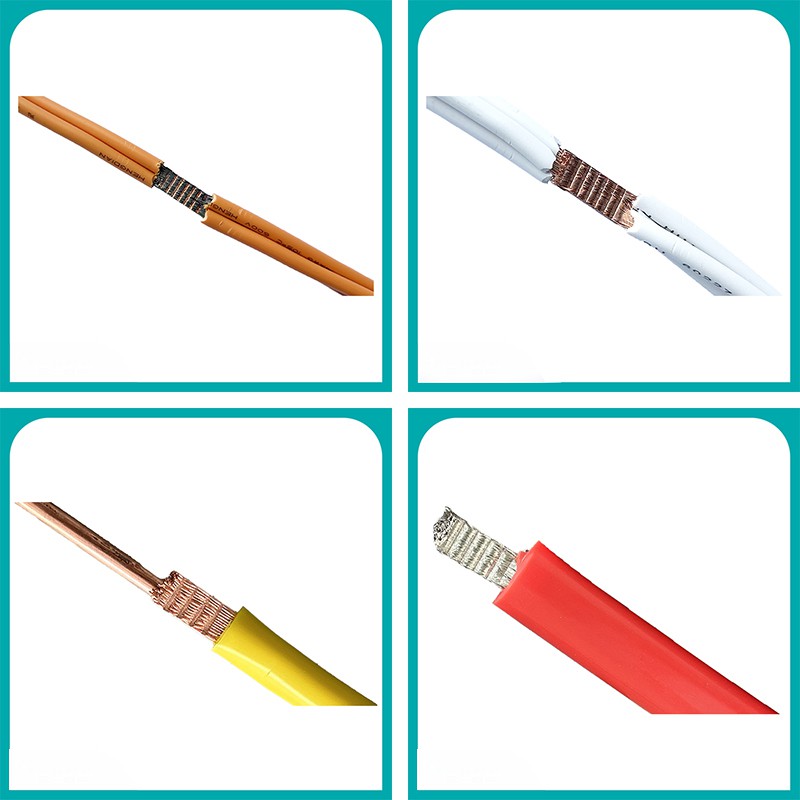
The ultrasonic metal welding machine converts electrical energy into high-frequency mechanical vibration above 20KHz through a transducer, creating solid-state metallurgical bonding at the metal contact surfaces under pressure. Compared with traditional crimping processes, this technology requires no metal melting and no flux, fundamentally eliminating failure modes associated with increased contact resistance and mechanical relaxation. From the perspective of Ultrasonic Welding vs Crimping for Wire Harness, ultrasonic welding demonstrates particularly outstanding advantages in copper-aluminum dissimilar metal connections, large cross-section wire harness welding, and high-vibration automotive environments.
This product series covers five power levels from 3000W to 12000W, with welding areas extending from 0.35mm² to 120mm², meeting the full range of application needs from precision sensors to energy storage copper-aluminum busbars. All equipment is certified under CE, FCC, and ISO systems, and features automation integration interfaces, providing standardized solutions for production line upgrades.
Technical Specifications: Full Series Parameter Comparison and Selection Basis
The table below summarizes the core parameters of the current main models. Procurement teams can perform preliminary matching based on wire diameter range, workshop space, and production capacity requirements. All data comes from factory measurements, ensuring accuracy in technical selection.
| Model | Power | Welding Area | Weight | Dimensions | Application Scenarios |
|---|---|---|---|---|---|
| YN-P203-F | 3000W | 1-100mm² | 73KG | 565×269×442mm | Precision electronics, sensors |
| YN-X203-Y | 3000W | 0.35-20mm² | 88KG | 670×520×410mm | High-efficiency precision metal welding |
| YN-X204-Z | 4000W | 1-30mm² | 132KG | 1020×610×1200mm | Lithium battery pack wire harnesses |
| YN-X206-Z | 6000W | 10-50mm² | 118KG | 1020×610×1200mm | Traction battery high-voltage wire harnesses |
| YN-D206-G | 6000W | 15-50mm² | 192KG | 1400×760×2000mm | High-voltage wire harness copper-aluminum terminals (split type) |
| YN-D208-G | 8000W | 20-70mm² | 957KG | 1750×1050×2150mm | Large wire harness copper-aluminum busbars |
| YN-D2012-G | 12000W | 35-120mm² | 988KG | 1750×1050×2150mm | Flagship welding for energy storage copper-aluminum busbars |
| JY-D204-F | 4000W | 1-35mm² | 82KG | 660×350×680mm | General copper-aluminum terminal welding |
Product Features: Core Technical Advantages and Engineering Value
Solid-State Welding Mechanism: Metallurgical Bonding Without Melting, Flux, or Spatter
During ultrasonic welding, the temperature at the metal interface does not exceed 50% of the material's melting point. High-frequency vibration removes surface oxide films and promotes atomic diffusion, forming a reliable solid-state metallurgical bond. This mechanism fundamentally avoids the porosity, slag inclusion, and heat-affected zone embrittlement issues associated with fusion welding, making it particularly suitable for scenarios where aluminum surface oxide layers are difficult to handle.
Electrical Performance: 30%-50% Reduction in Contact Resistance
Measured data shows that the contact resistance of ultrasonic weld points is significantly lower than that of crimped terminals. In the quantitative comparison of Ultrasonic Welding vs Crimping for Wire Harness, ultrasonic welding improves current-carrying capacity by approximately 40%, with lower temperature rise during continuous high-current flow, effectively extending the service life of wire harness assemblies.
Mechanical Strength and Long-Term Reliability
The tensile strength of weld points typically reaches over 80% of the base material strength, without the elastic relaxation issues common in crimping processes. In high-vibration automotive environments, ultrasonic weld points do not experience contact resistance drift due to fretting wear, and their long-term reliability far exceeds that of mechanical crimping.
Dissimilar Metal Connection Capability
Copper-aluminum dissimilar metal connection is a technical blind spot for crimping processes, whereas ultrasonic welding achieves direct bonding of copper and aluminum atoms through solid-state diffusion, requiring no transition pieces or special treatment. This capability holds irreplaceable value in new energy vehicle battery connections and energy storage copper-aluminum busbar welding.
Automation Integration and Production Line Adaptation
The full series supports PLC communication interfaces, robot linkage, and rotary-table multi-station integration. The split-type model YN-D206-G (1400×760×2000mm) can be flexibly embedded into existing production lines, while the integrated model YN-D2012-G (1750×1050×2150mm) is suitable for standalone workstation layouts.
Application Scenarios: Field Validation from Precision Sensors to Energy Storage Copper-Aluminum Busbars
- New Energy Vehicle High-Voltage Wire Harnesses:The YN-X206-Z (6000W, welding area 10-50mm²) is specifically designed for traction battery high-voltage wire harnesses, delivering stable performance in battery pack internal connections and motor controller terminal welding, with weld consistency meeting IATF 16949 system requirements.
- Energy Storage System Copper-Aluminum Busbar Connections:The YN-D2012-G (12000W, welding area 35-120mm²), as the flagship model of the D series, achieves a productivity advantage of less than 3 seconds per weld point in large cross-section copper-aluminum busbar welding, matching the high-speed production cadence of energy storage modules.
- Consumer Electronics and Precision Sensors:The YN-P203-F (3000W, welding area 1-100mm², weight 73KG) meets the precision requirements of micro wire diameter welding with its compact body and precise amplitude control, suitable for internal lead connections in sensors.
- Large Commercial Vehicle Wire Harnesses:The YN-D208-G (8000W, welding area 20-70mm²) has validated its reliability in long-term vibration environments for commercial vehicle chassis wire harness copper-aluminum busbar welding, with a machine weight of 957KG ensuring stability during the welding process.
FAQ: Frequently Asked Questions About Ultrasonic Welding and Crimping Processes
Can ultrasonic welding completely replace crimping processes? Where are the application boundaries?
Ultrasonic welding shows clear advantages in copper-aluminum connections, large cross-section wire harnesses, and high-vibration scenarios, but crimping processes still hold advantages in extremely fine wire diameters (<0.1mm²
Does aluminum wire harness welding face oxide layer treatment challenges? How does ultrasonic welding solve this?
The oxide layer on aluminum surfaces is a major pain point for crimping processes. Ultrasonic welding mechanically breaks the oxide film through high-frequency vibration and maintains fresh metal surface contact under pressure, requiring no chemical cleaning or flux, fundamentally solving the oxide layer problem in aluminum welding.
How low can the contact resistance of ultrasonic weld points go?
According to factory measured data, the contact resistance of ultrasonic weld points is 30%-50% lower than that of crimped terminals, with specific values depending on material combinations and welding parameters. We recommend that procurement teams provide actual wire diameter specifications for sample welding tests by our engineering team.
What welding scenarios is the 12000W model suitable for?
The YN-D2012-G (12000W, welding area 35-120mm²) is specifically designed for energy storage copper-aluminum busbars and ultra-large cross-section wire harnesses. Its 988KG body ensures mechanical stability during high-power output, making it suitable for heavy-duty connection scenarios such as energy storage modules and power electronics cabinets.
How should split-type and integrated structures be selected?
Split-type models (such as YN-D206-G, 1400×760×2000mm) separate the generator from the welding head, making them suitable for embedding into existing production lines or space-constrained workstations; integrated models (such as YN-D208-G, 1750×1050×2150mm) have a compact structure and are suitable for standalone workstations.
Does the equipment support automated production line integration?
The full series comes standard with PLC communication interfaces, supporting I/O signal control, RS485/Ethernet communication, and seamless integration with robots, rotary tables, and conveyor lines. Specific integration solutions need to be confirmed based on production line layout.
How is weld quality inspected?
The standard inspection process includes metallographic analysis (observing the metallurgical bond layer), tensile testing (verifying tensile strength), and contact resistance testing (confirming electrical performance). We can provide inspection method training and recommendations for supporting inspection equipment selection.
What is the equipment energy consumption level?
Ultrasonic welding uses short-pulse energy output. Taking the 6000W model as an example, energy consumption per weld is approximately 0.01-0.03kWh, saving over 70% energy compared to resistance welding. Specific energy consumption depends on welding area and material thickness.
What is the mold lifespan and replacement cost?
Standard mold lifespan is 100,000-300,000 welds, depending on material hardness and welding area. Mold replacement uses a quick-change design, with each replacement taking no more than 10 minutes, and spare parts supply lead time is 3-5 working days.
What is the equipment certification status?
The YN-X203-Y model has passed CE, FCC, and ISO certification, and the full series is manufactured in accordance with the ISO 9001 quality system. For industry-specific certifications (such as IATF 16949), relevant supporting documents can be provided.
How reliable is copper-aluminum dissimilar metal welding?
Copper-aluminum ultrasonic welding forms an intermetallic compound layer through solid-state diffusion, with thickness controlled at 1-2μm and stable bond strength. After thermal cycling tests from -40°C to +125°C, the contact resistance change rate is less than 5%.
How long is the equipment operation training period?
The standard training period is 2-3 days, covering equipment operation, parameter setting, routine maintenance, and troubleshooting. After training, operators can independently complete welding parameter adjustments and quality self-inspection.
How is the correspondence between welding area and wire diameter determined?
The correspondence between welding area and wire diameter must be determined comprehensively based on wire harness cross-sectional area, strand count, and material type. For example, 35mm² copper busbars are recommended for the YN-D2012-G (welding area 35-120mm²), while 0.5mm² fine wires are suitable for the YN-P203-F (welding area 1-100mm²).
What is the equipment maintenance cycle and content?
It is recommended to check the transducer connection bolt torque every 5,000 welds and replace the amplitude transformer lubricating grease every 20,000 welds. The equipment comes standard with a fault self-diagnosis system that monitors amplitude, frequency, and temperature parameters in real time.
Is it complicated to convert a production line from crimping to ultrasonic welding?
The conversion involves workstation layout adjustments, electrical interface matching, and operator training, typically completable within 1-2 weeks. We provide production line assessment services, offering solutions that minimize conversion costs based on existing crimping equipment layouts.
What is the equipment warranty policy and after-sales response time?
The standard warranty period is 12 months, with core components (transducer, amplitude transformer) warranted for 24 months. The after-sales service network covers major industrial cities nationwide, with emergency fault response times not exceeding 24 hours.
Qualifications and Contact: Certification System and Technical Support
The full series of ultrasonic metal welding machines is developed and manufactured in accordance with the ISO 9001 quality system. The YN-X203-Y model has passed CE, FCC, and ISO certification, ensuring compliance with international standards in electromagnetic compatibility, radiation safety, and quality management. For automotive industry customers, we can assist in completing equipment validation documentation required for IATF 16949 system audits.
If you are evaluating an Ultrasonic Welding vs Crimping for Wire Harness process upgrade solution, please provide your specific wire diameter range, material combinations, and production cadence requirements. Our engineering team will complete sample welding tests and equipment selection matching for you. For non-standard automation integration needs, please confirm interface protocols and production line layout plans with our technical department.
Wire Harness Assembly
Need matched harnesses?
Genuine connectors plus our own harness factory: crimping, overmolding and electrical testing — consignment or full supply.
Comments (0)
Loading…